Sep 24, 2026Buying Guides
60L Red Copper Distiller: How To Make Essential Oil & Hydrosol By Steam Distillation
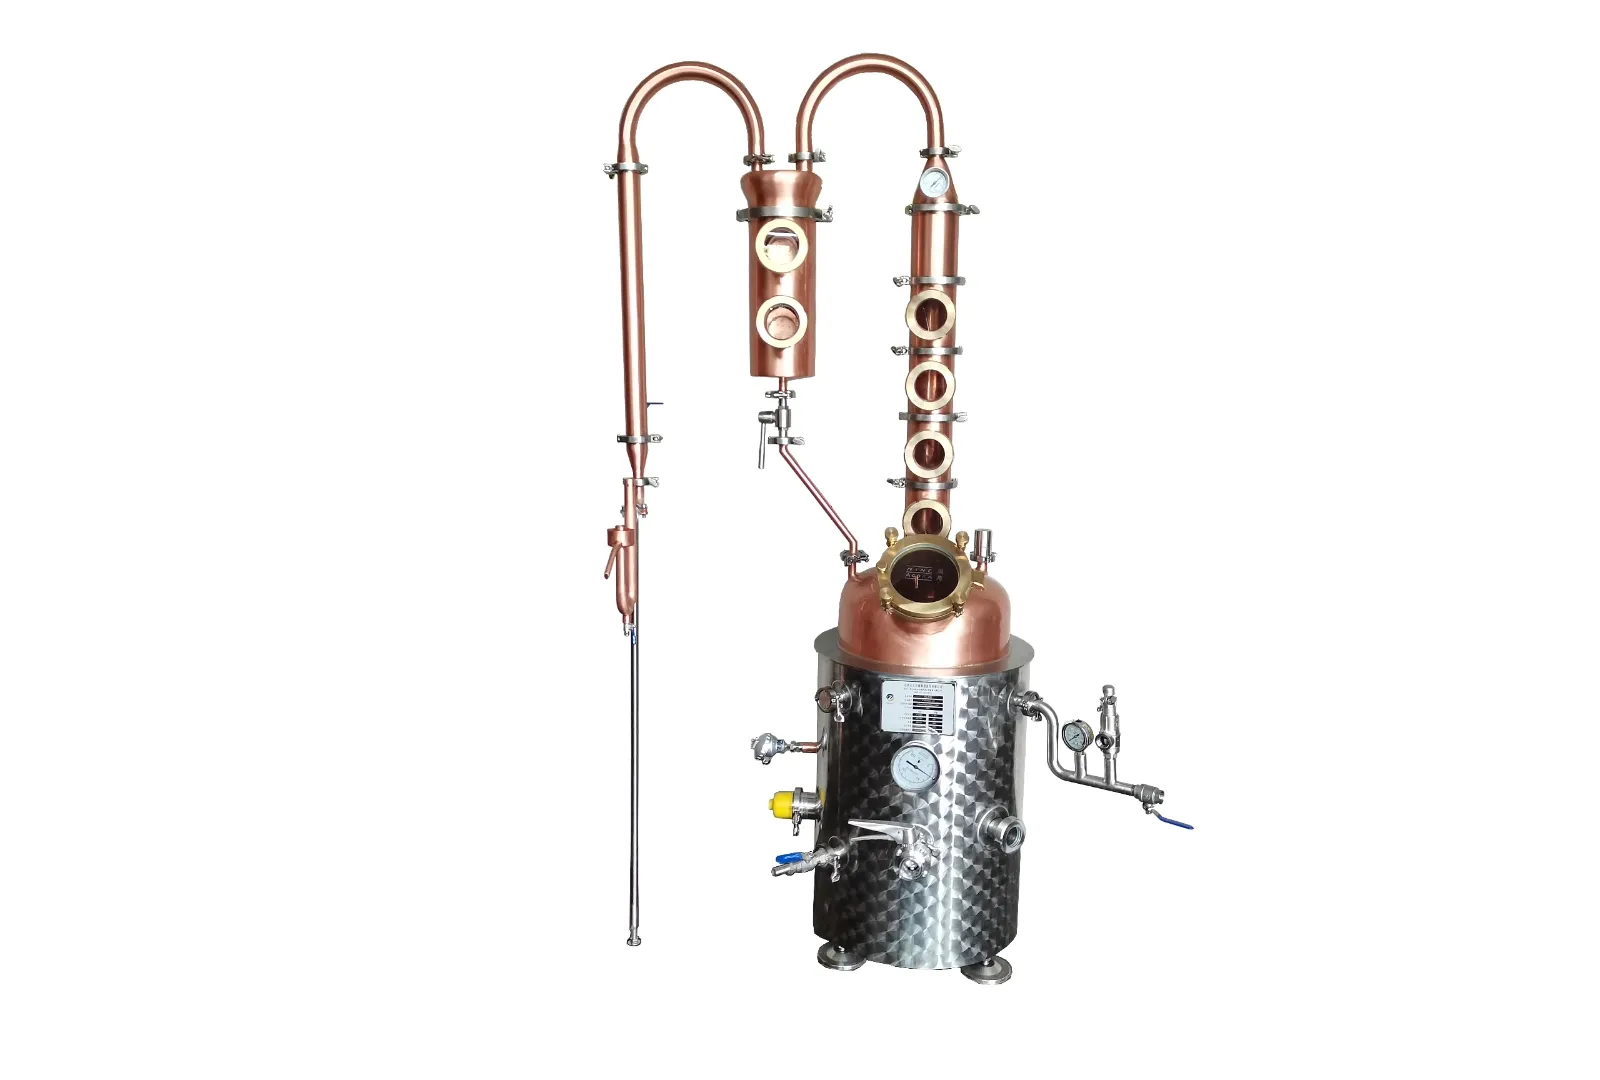
This 60L food-grade red copper distiller is built for small batch steam distillation to extract essential oil and hydrosol from roses, lavender, jasmine and aromatic herbs.
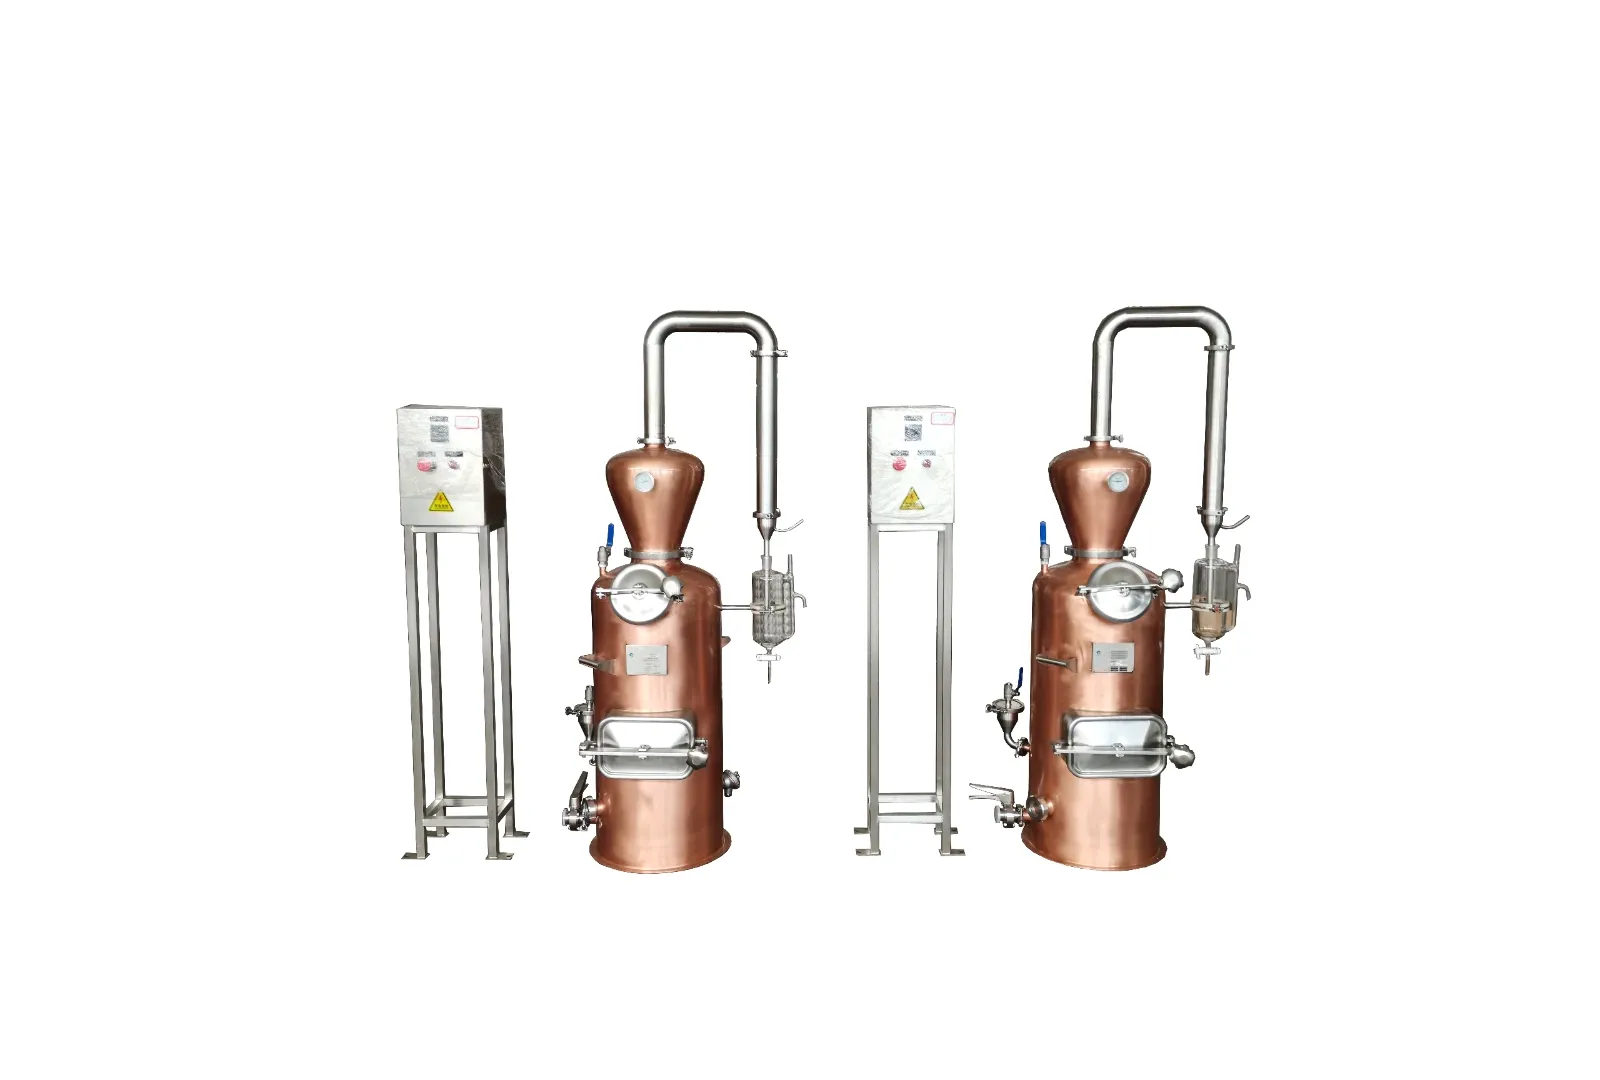
Ingenious Extraction, Copper Leads the Future — 100L Red Copper Distillation Equipment for Essential Oil & Hydrosol
It is my great honor to stand here today to discuss equipment upgrading and quality breakthroughs within the aromatics industry. As "returning to nature" becomes a shared pursuit across cosmetics, aromatherapy and the greater health markets, demand for hydrosol and essential oil is growing at an impressive rate. Yet rising market expectations impose stricter requirements on extraction processes: how can we fully preserve the soul of botanicals? How can we strike a balance between mass production and consistent quality?
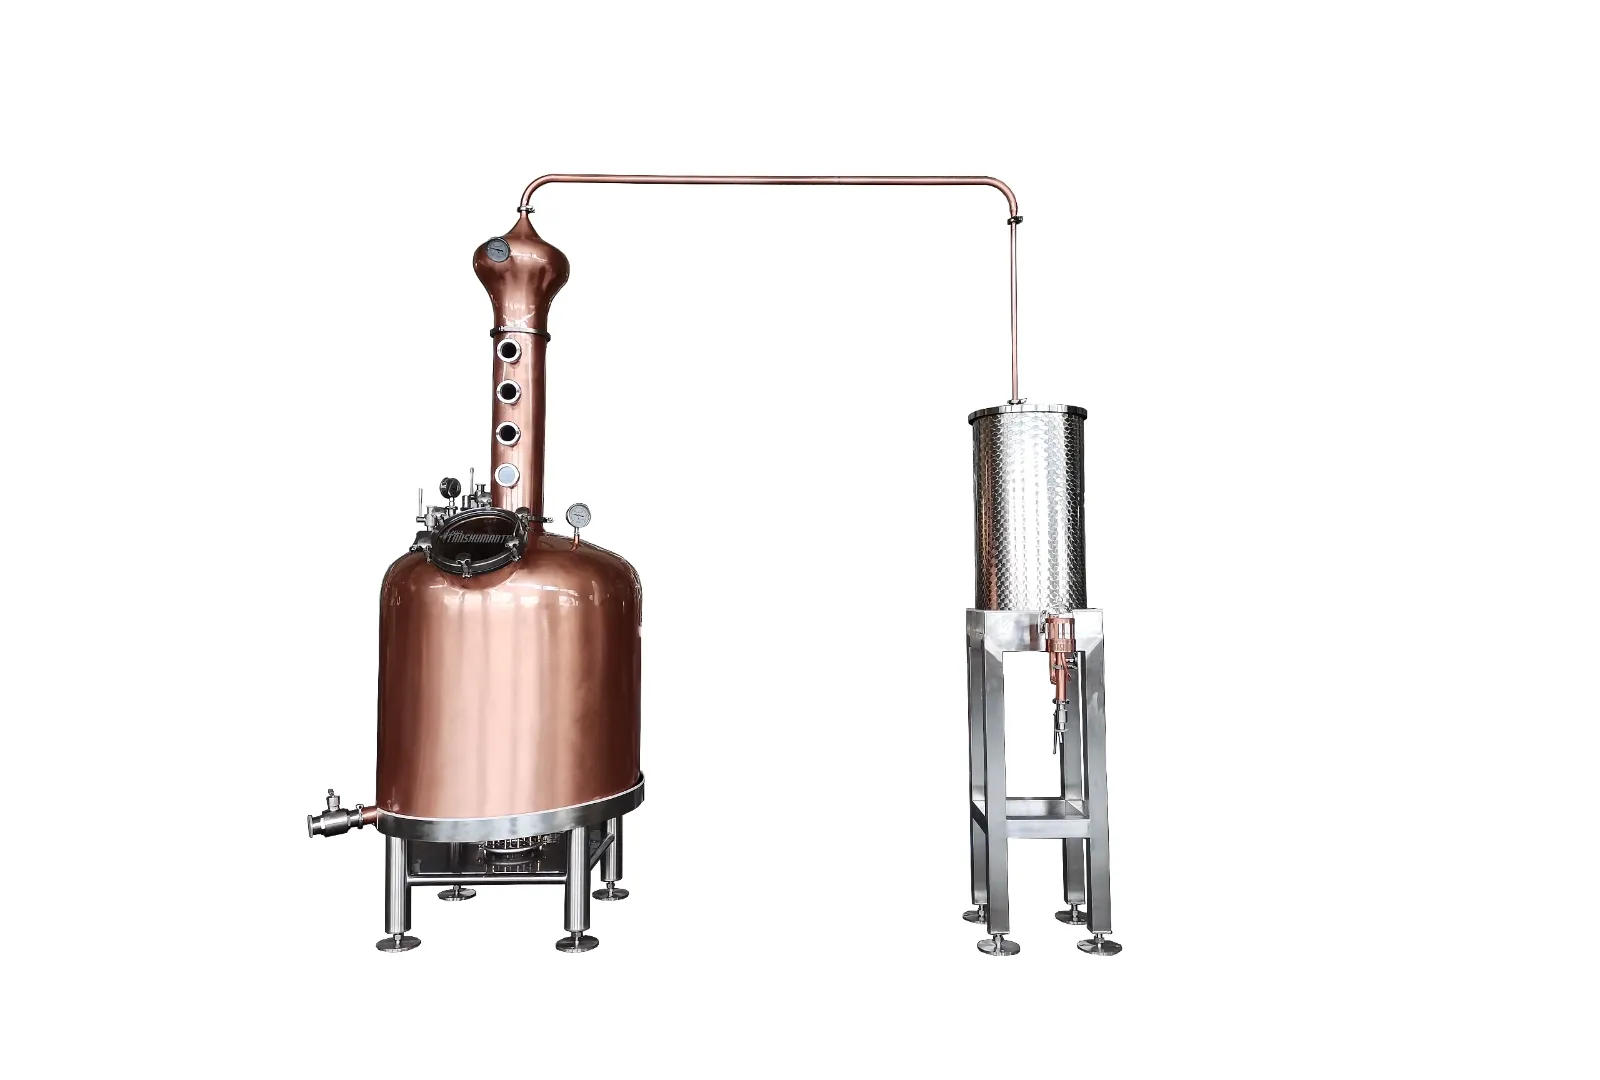
Today, I am proud to present our meticulously crafted solution built to address these pain points — the 100L Red Copper Distillation Equipment for Essential Oil & Hydrosol.
Why red copper? Why 100L capacity? This is more than a simple choice of material and volume; it represents the deep integration of traditional wisdom and modern manufacturing technology.
First, red copper is the gold standard for aromatic extraction. Within distillation, the advantages of red copper are irreplaceable.
- Red copper delivers exceptional thermal conductivity. It heats up rapidly and enables precise temperature control, greatly shortening distillation cycles while cutting energy consumption.
- Red copper features natural antibacterial and anti-corrosion properties, safeguarding the purity of your distillate and extending equipment service life. Most importantly, at high temperatures, red copper triggers mild reactions with impurities such as sulfides released from plant materials, effectively removing off-notes. This yields essential oils with richer, more radiant aroma and fresh, crystal-clear hydrosol. This unique chemical interaction between metal and botanicals cannot be achieved by stainless steel stills.
Second, the 100L golden capacity hits the sweet spot balancing quality and profitability. For mid & small aromatherapy brands, botanical planting bases and premium SPA centers, undersized equipment suffers from low productivity and struggles to meet commercial needs. Overly large units carry high raw material costs per batch, risk resource waste and inconsistent batch quality. The 100L capacity serves as the ideal transition from lab-scale handmade trials to standardized commercial production. It processes dozens of kilograms of floral raw materials per batch with stable and controllable oil and hydrosol yields. It maintains consistent quality across every batch, while giving operators flexible production scheduling and faster capital turnover.
Lastly, refined details bring professional performance within reach. Beyond material and capacity, we spared no effort in perfecting every detail of this unit. We adopt food-grade welding technology to ensure seamless surfaces with no dead corners for easy cleaning. It is equipped with a high-efficiency condensation system that greatly boosts oil-water separation efficiency and prevents loss of highly volatile aromatic compounds. Meanwhile, flexible reserved ports and intelligent temperature controllers are fitted. One single machine can easily adapt to the characteristics of different plants via steam distillation, hydrodistillation or water-and-steam distillation.
Dear colleagues, a distiller is not merely a cold vessel. It is a bridge that transforms plant life forms. Our motivation for launching this 100L red copper distillation equipment is to allow new aromatherapy startups to access premium extraction quality right from the beginning, and help growers turn their flowers and herbs into high-value "liquid gold".
Extract the soul of botanicals, fulfill the beauty of nature. We look forward to this 100L red copper distiller becoming your reliable partner on your aromatic journey. Together, let us distill premium hydrosol and authentic essential oil!